In abrasive waterjet cutting, mixing tube (nozzle) replacement represents a significant operating cost. Choosing high-quality garnet abrasive is the most effective way to extend nozzle life and maintain cutting precision. Focus on three critical factors:
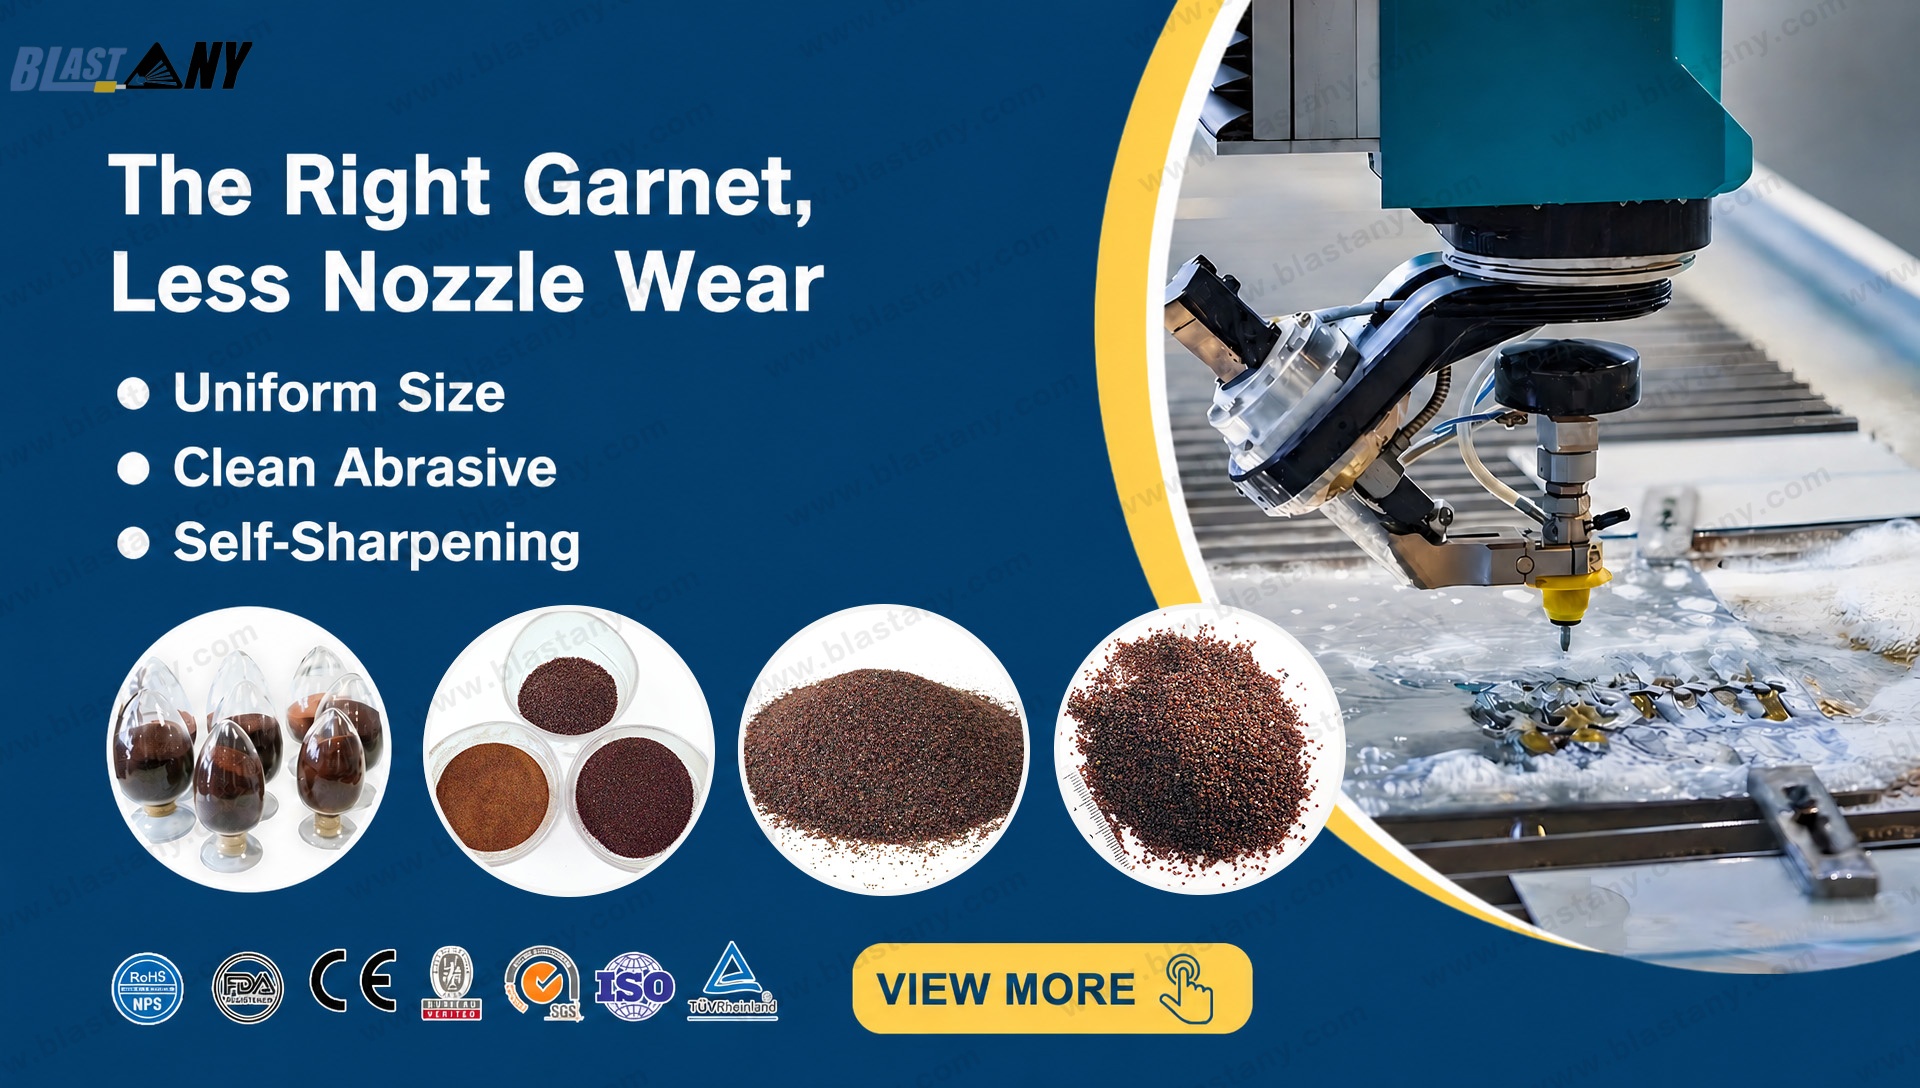
Particle Size & Consistency: Uniform grain distribution is vital. Oversized particles cause rapid orifice and mixing tube erosion, while erratic sizing leads to frequent nozzle clogging. Matching the exact mesh size (e.g., 80 mesh) to your focusing tube diameter ensures steady flow and balanced abrasive kinetic energy.
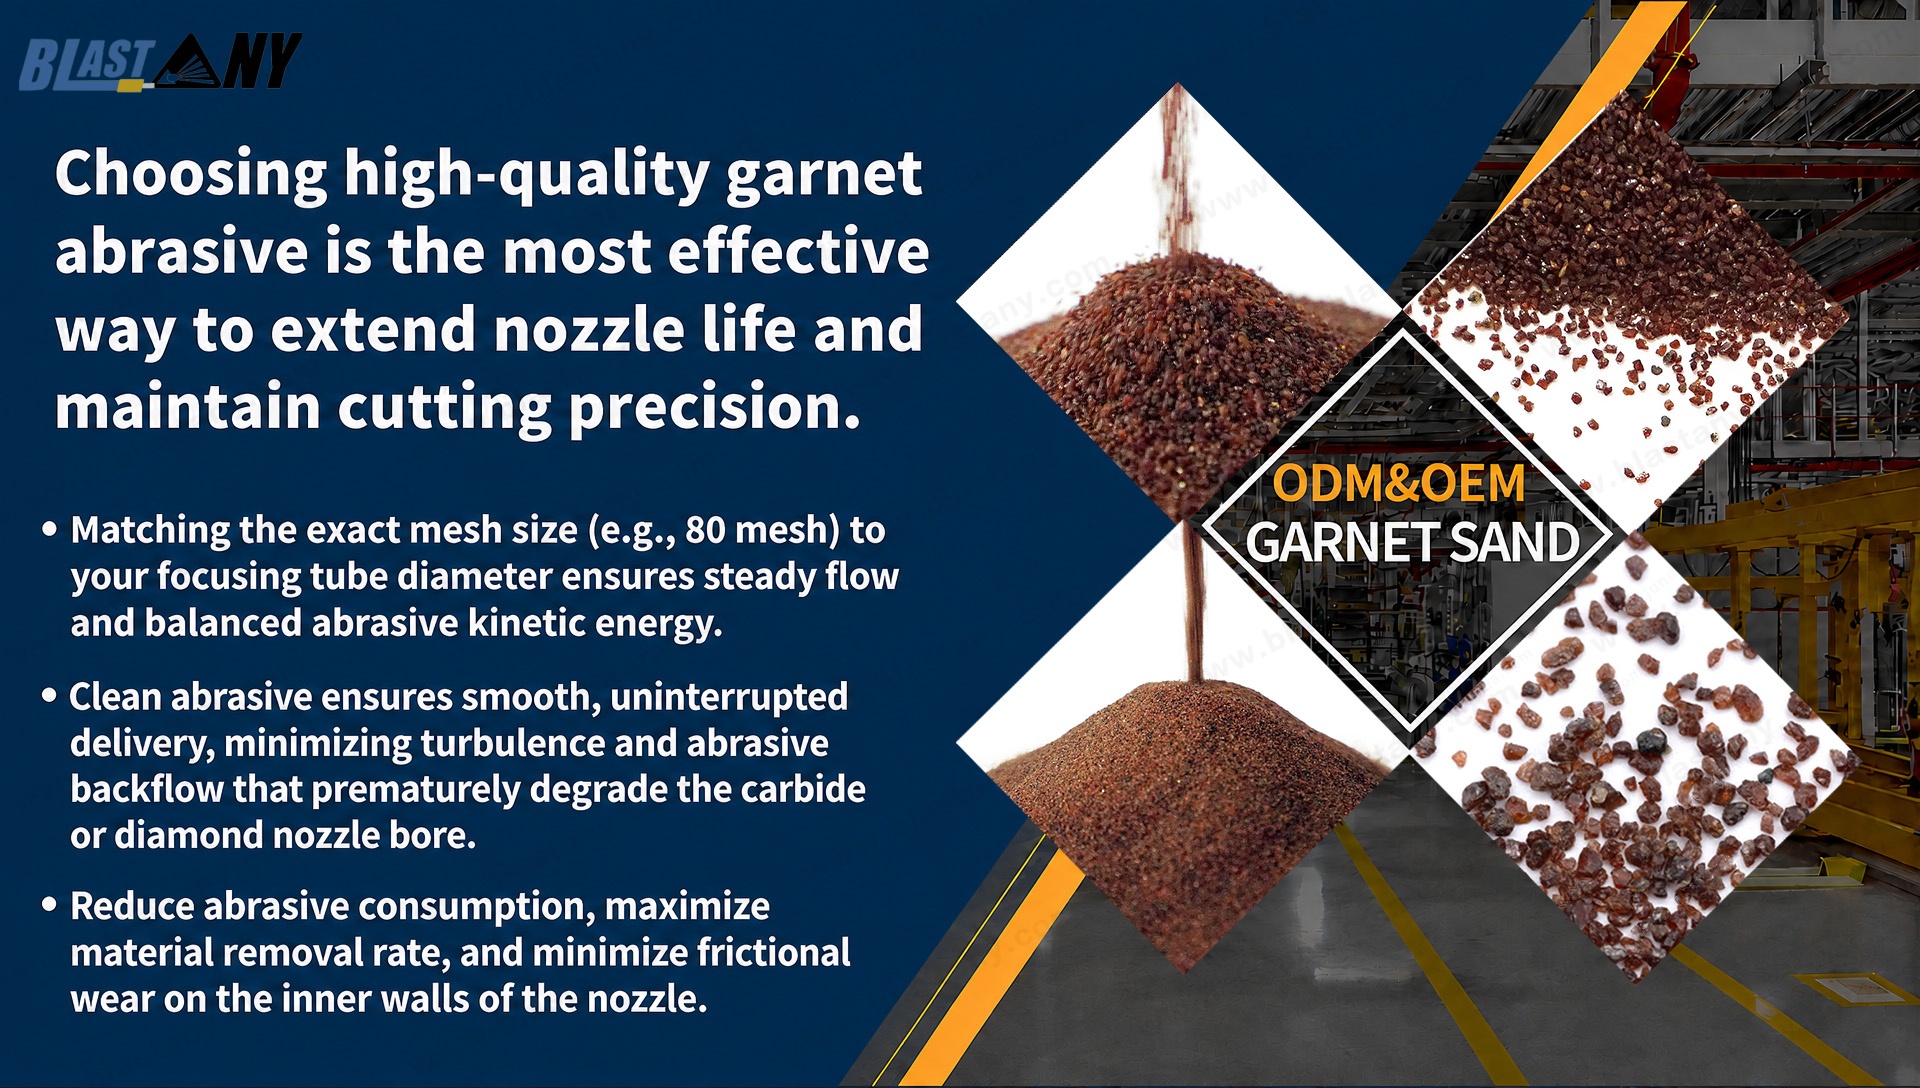
Abrasive Cleanliness: High-purity garnet free of dust, clay, and chlorides prevents slurry blockages in the cutting head. Clean abrasive ensures smooth, uninterrupted delivery, minimizing turbulence and abrasive backflow that prematurely degrade the carbide or diamond nozzle bore.Self-Sharpening Sharpness: Premium almandine garnet fractures along natural crystalline planes, continuously exposing sharp cutting edges without shattering into useless dust upon impact. This self-sharpening behavior maximizes material removal rates at lower abrasive consumption, reducing frictional wear on internal nozzle walls.
Optimizing these three properties directly lowers consumable costs and minimizes machine downtime.
Our garnet sand 80A+ is the ideal waterjet cutting media for your choices.
Post time: Oct-22-2026


